P05 MagSafe Car Vent Phone Mount: four printed parts, one modeled thread, one caught drawing error
A four-part car air-vent phone mount for MagSafe phones. The drawings were prepared in Gearhed's title block and treated like client prints. I modeled each part in Onshape from the drawings and printed the parts in ASA or PETG on my Creality K2 Plus. (Practice project: an original drawing set, not a client job and not my own from-scratch design.)

The package
Four drawing sheets, one per part, all printed in ASA or PETG:
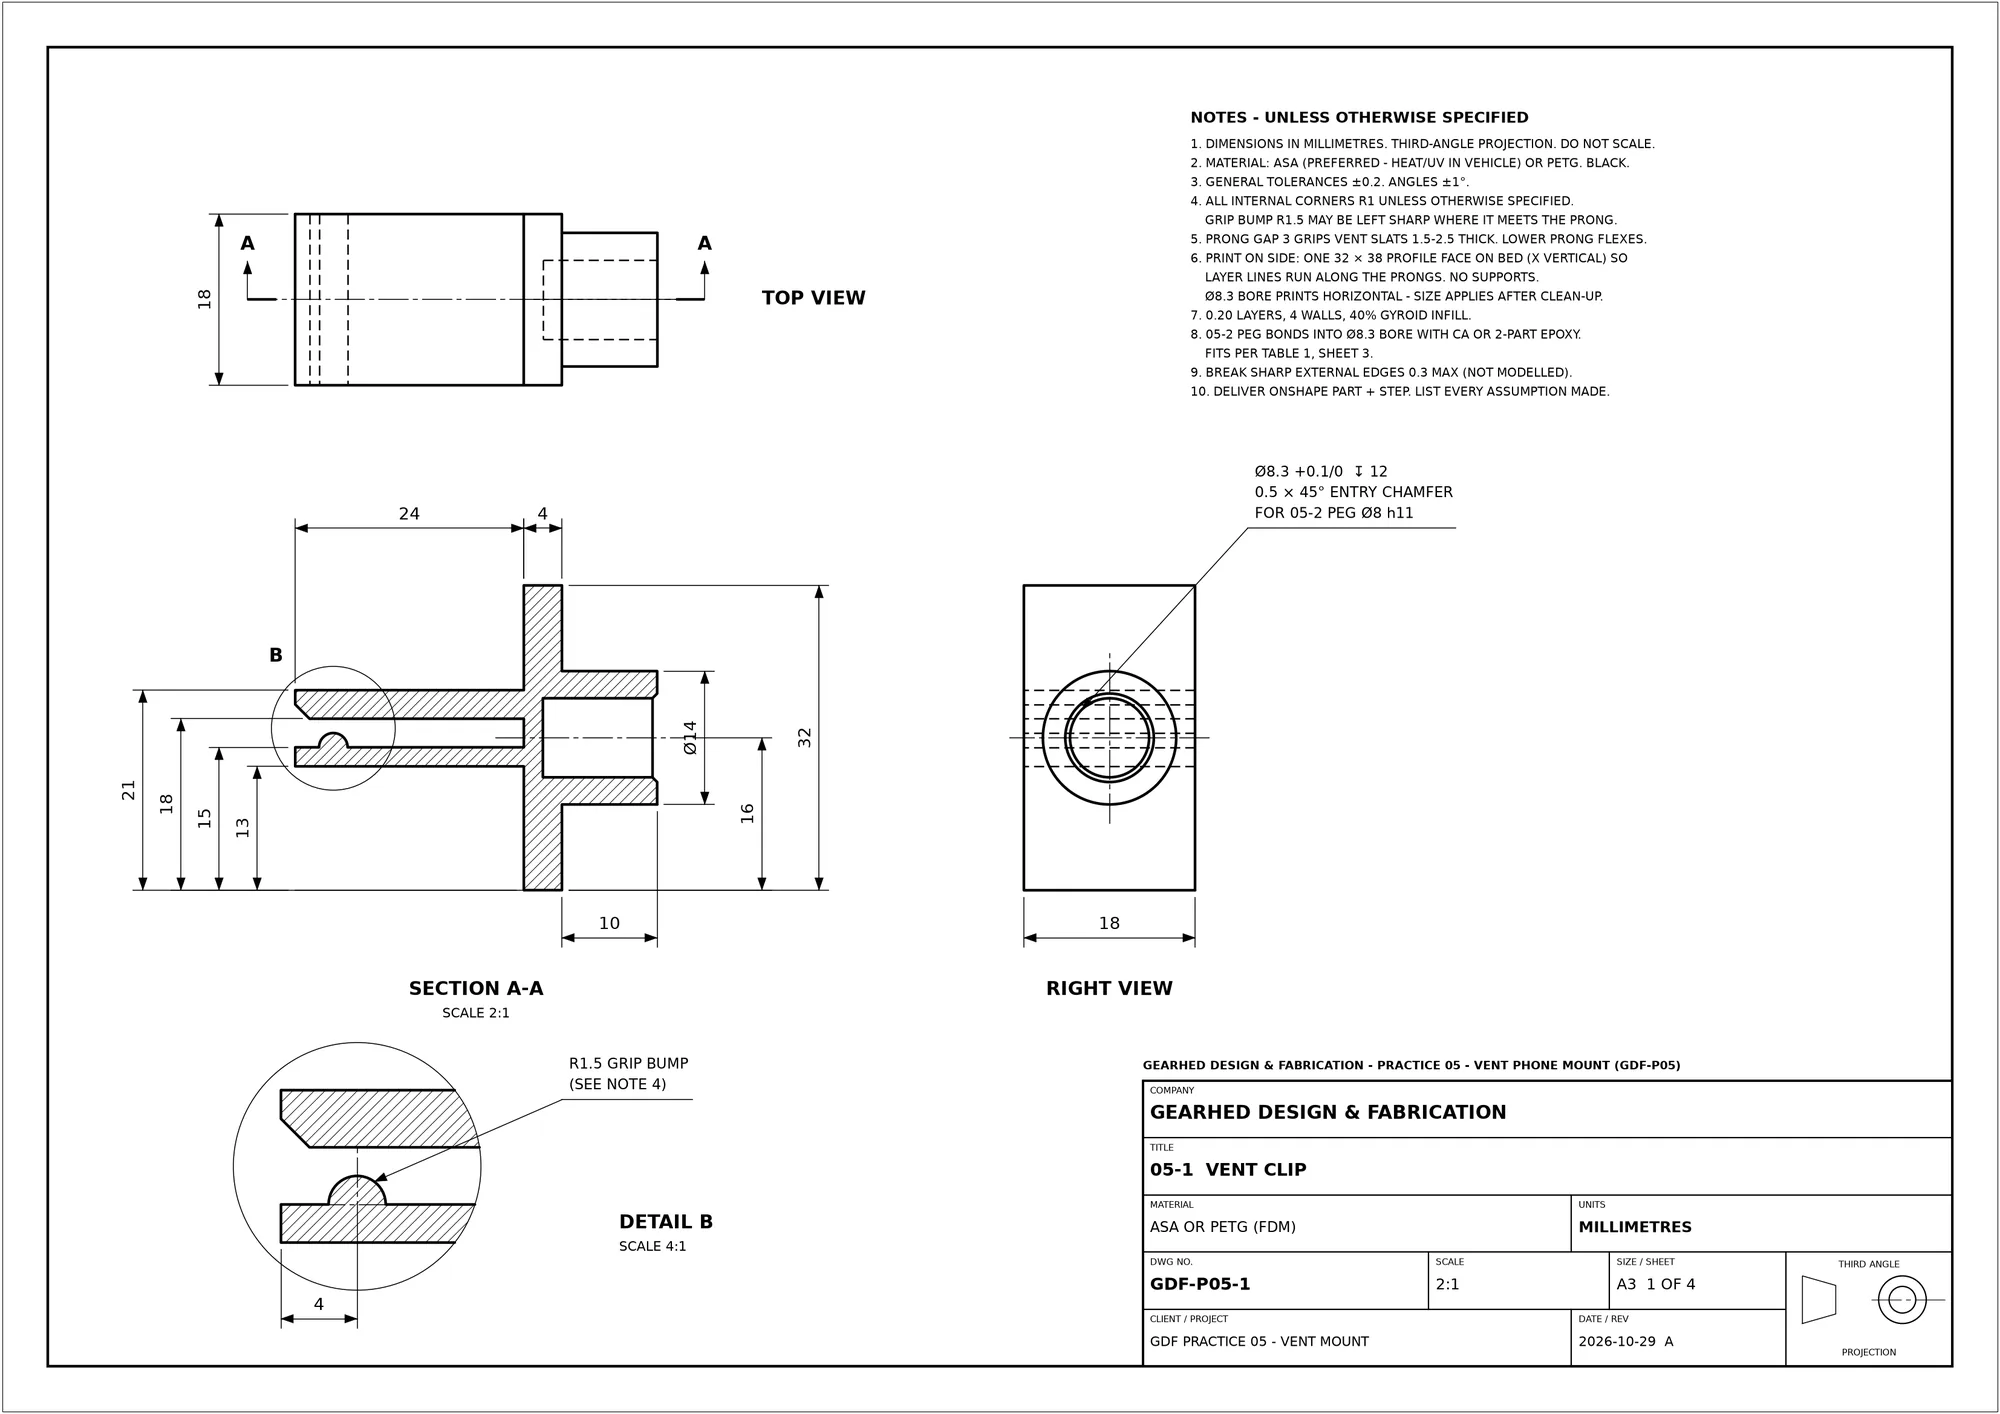
- 05-1 Vent clip: a two-prong clip for the vent slat, with a flexing lower prong and a grip bump, and a Ø14 boss with a blind bore for the arm. The drawing uses section and hidden views, a 4:1 detail, and fillets set by a general note.
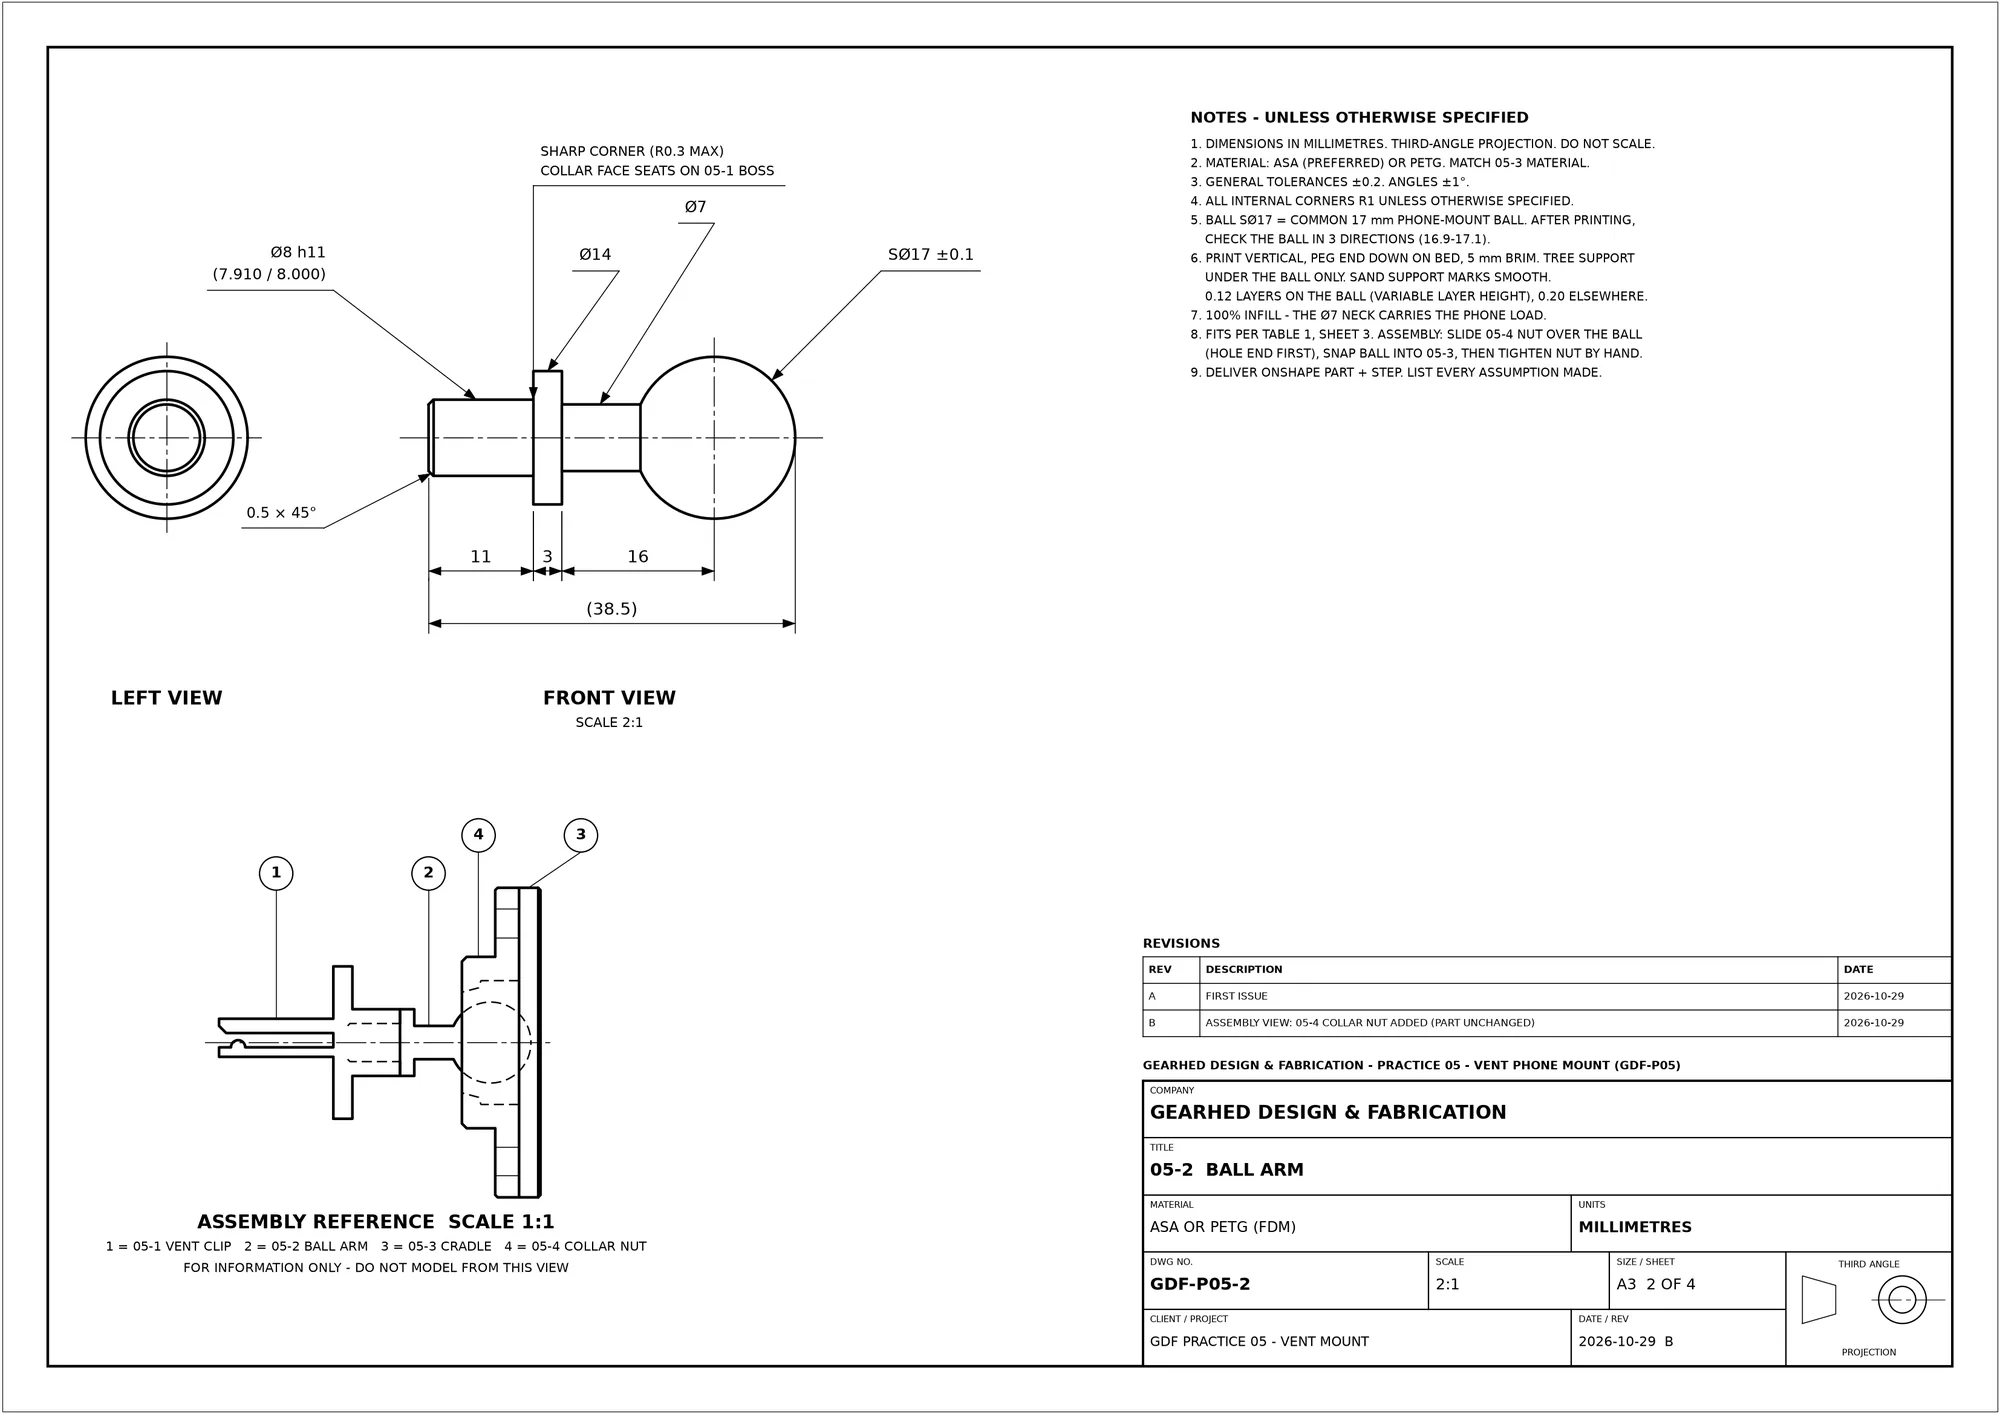
- 05-2 Ball arm: a revolved part with an Ø8 peg (h11 fit, given with its limits), a collar, a Ø7 neck and an SØ17 ball.
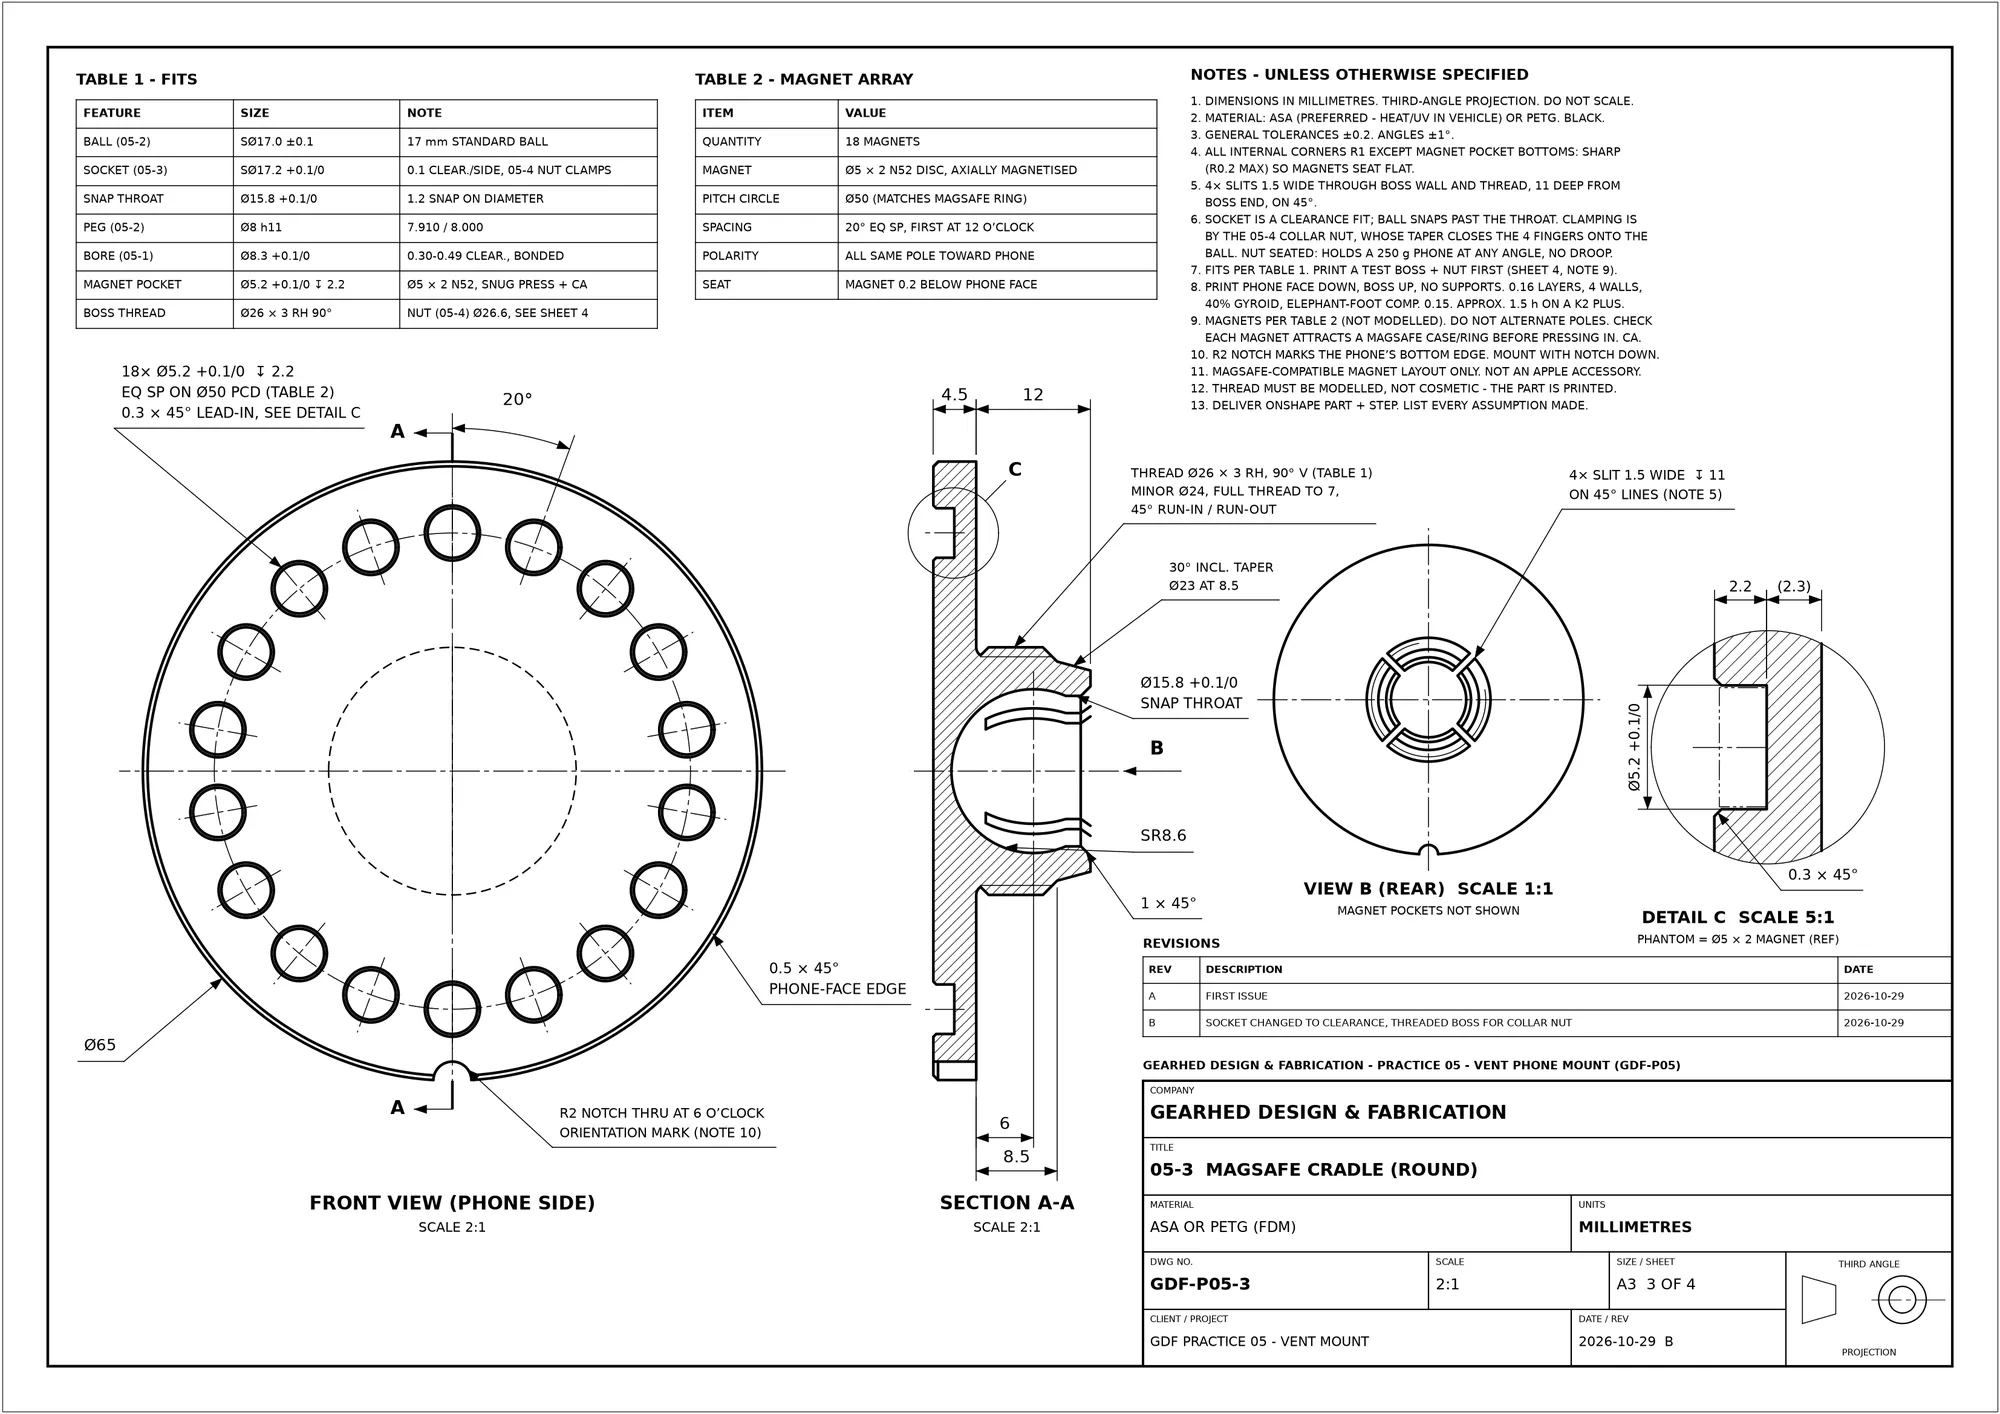
- 05-3 MagSafe cradle: a Ø65 disc with a ring of Ø5×2 disc magnet pockets on a pitch circle for MagSafe alignment, and an SØ17.2 (SR8.6) clearance socket for the ball. The slotted back boss carries a custom 90° V thread, 26 mm with a 3 mm pitch.
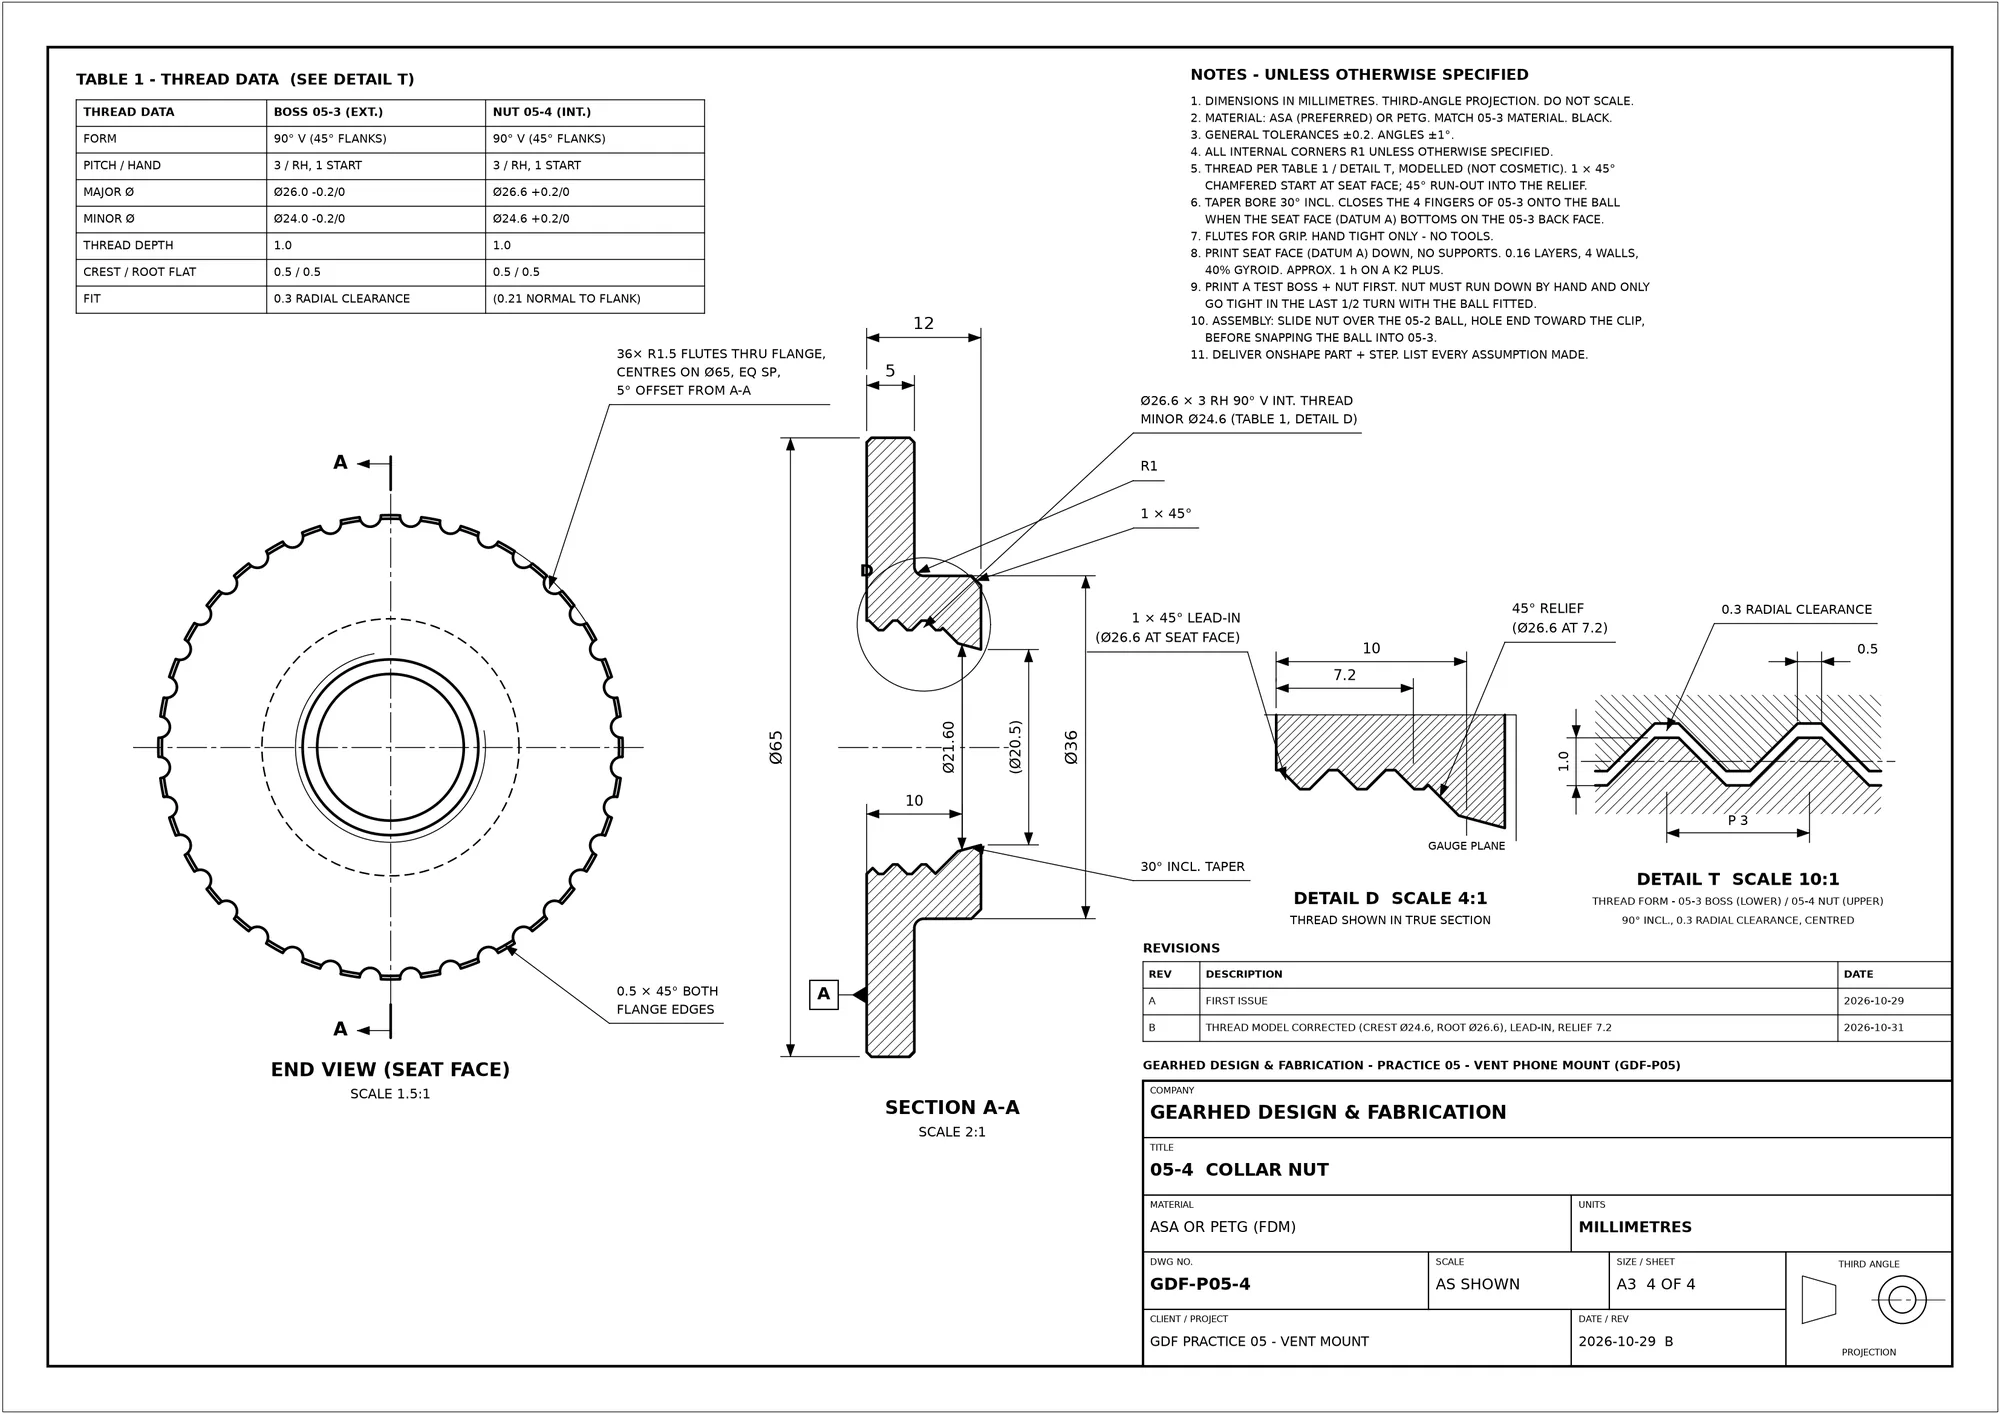
- 05-4 Collar nut: a Ø65 fluted nut, 12 thick, with 36 flutes and a matching internal thread (crest Ø24.6, root Ø26.6, P3 RH). Its 30° tapered bore squeezes the four boss fingers onto the ball to lock the angle.
The drawing sheets
Original practice drawing package (GDP-P05). Sheet 05-4 is shown at Rev B, after the Oct 31 correction. Select a sheet to open it full size.
The models
My Onshape models, exported to STEP and rendered.


What I did
- Read every view and note. The vent clip's section and hidden views, its 4:1 detail, and the fillets that appear only in a general note were all modeled.
- Kept turned parts as revolves. The ball arm is one revolved profile: the Ø8 h11 peg, the collar, the Ø7 neck and the SØ17 ball.
- Modeled the thread, not just a cosmetic callout. The cradle's 90° V thread (26 mm, 3 mm pitch) is a real helix sweep, with a loft for the thread start, so it prints as a working thread. The collar nut carries the matching internal thread.
- Printed it and tested the fit. On Oct 31, a K2 Plus test print showed the nut wouldn't engage the cradle thread. The cause was a design error in the original drawing and reference model, not in my model: the nut's minor diameter sat outside the boss crest. I flipped the thread profile, the reprint meshed, and the drawing was corrected to Rev B.
- Checked the clamp. PETG test prints confirmed the roughly 0.3 mm clamp squeeze from the nut's tapered bore grips the ball well.
- Documented every deviation. No seat-side flange chamfer on the nut (for looks), the flutes aren't rotated 5°, and all edges are broken for printing.
Result
The rebuilt collar nut matched the reference model's volume within 0.02%, and the corrected thread meshed on the reprint.
Why it matters for your job: Sometimes the drawing is what's wrong. Here a test print exposed a thread error in the original drawing, and the fix went back into the drawing as Rev B, not just into one part.